
TPE Overmold Adhesion Testing: Peel Strength, Failure Modes, and Validation
How to run TPE overmold adhesion testing: repeatable peel tests, adhesive and cohesive failure modes, conditioning effects, and revalidation triggers.
How to run TPE overmold adhesion testing: repeatable peel tests, adhesive and cohesive failure modes, conditioning effects, and revalidation triggers.
A color approval workflow for injection molding that holds in production: master standards, viewing conditions, Delta E limits, and drift diagnosis.
A complete T1 sample package pairs cavity-traceable parts with preserved process data and tool records, so first-shot results can be explained and repeated.
Learn how to judge thin wall injection molding feasibility using flow-length ratios, machine pressure and flow margins, clamp force, and mold stiffness.
How steel-safe mold design keeps critical dimensions correctable after T1, with planned removal direction, sized correction stock, and a T1 correction loop.
Learn why molded parts pass inspection at the press but fail later, and how to run a time-signature study and standardize measurement conditions.
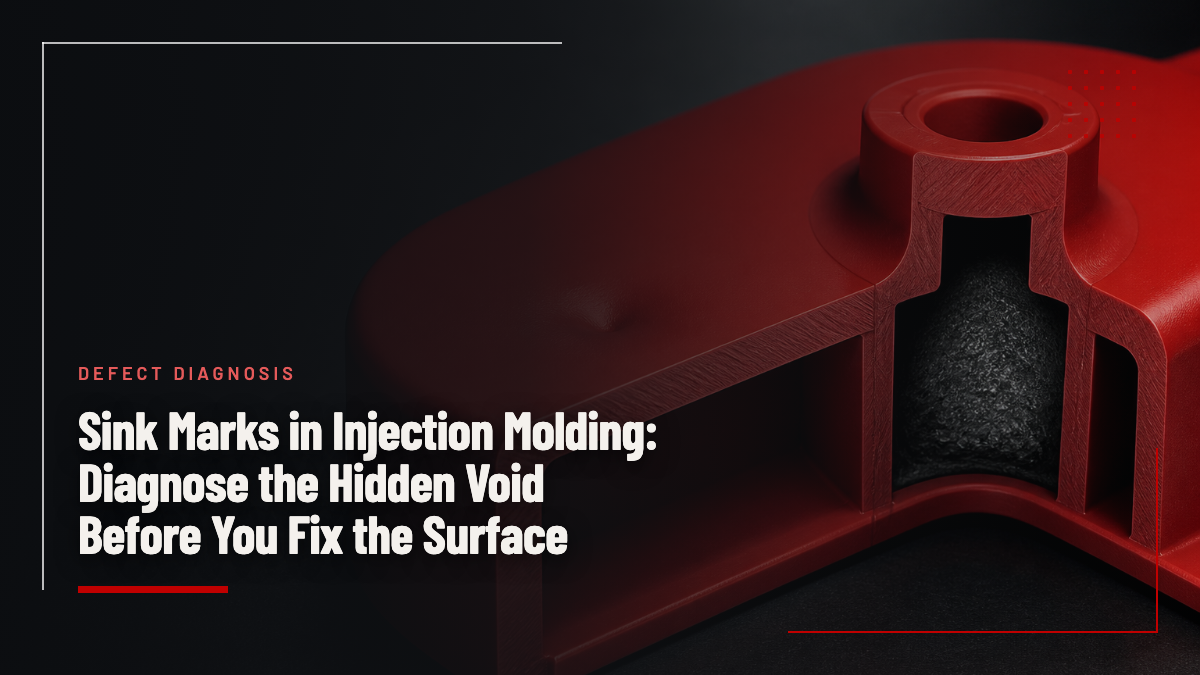
How to tell a surface sink, a shrinkage void, and a gas bubble apart, and why a better surface can hide a worse interior in molded parts.
How to prove resin is dry before injection molding: measure moisture at the feed point, control drying variables, and separate symptoms from damage.
How to tell static tool offset, mold deflection, and dynamic core bending apart when a molded part shows uneven wall thickness.
How to qualify PBT for electrical parts: verify UL 94 at actual wall thickness, CTI, glow-wire performance, drying, and regrind rules per grade.